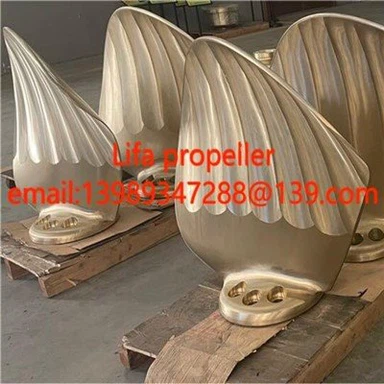
Surface Treatment Of Ship Propeller Blades
Feb 07, 2023
Correction process of ship propeller blade bending:
1. Condition correction: for bending with edge thickness less than 30mm, the heating temperature can be below 205 ℃ for correction. The parts with thin section and small bending can be corrected by hammering, twisting and jacking.
2. Hot correction: when the bending degree or area of the blade is large, the hot correction should be adopted. Both dynamic and static load correction methods can be used. The heating temperature shall pass through the whole section thickness of the correction point and be maintained until the correction ends.
3. Stress relief annealing treatment: after severe bending or large area correction, stress relief annealing treatment shall be taken according to material characteristics. Generally, the annealing requirements of nickel-aluminum bronze blades can be reduced.
4. Inspection after correction: dye penetrant inspection shall be carried out for blade bending after correction, and any cracks and uneven defects found shall be repaired. If the correction area is large, the pitch shall be measured again.
Surface polishing treatment of propeller blade:
1. Polishing is required to remove the dirt on the blade surface or improve the smoothness of the blade surface. Whether the blade is repaired by welding or bending correction, it shall be polished.
2. Polishing can be divided into two steps: rough polishing and fine polishing; Rough polishing is made of 24 # - 80 # paper grinding wheel; 100 # - 120 # cloth grinding wheel is used for fine polishing.